
The medical device manufacturing sector demands uncompromising precision, safety, and efficiency. Among these, the 5ml medical syringe barrel stands out as a classic high-precision, thin-walled medical component.
Achieving flawless high-volume production requires a deep understanding of product geometry, material behavior, and potential defect mitigation. Let's break down how to optimize the injection molding process for this critical medical component.
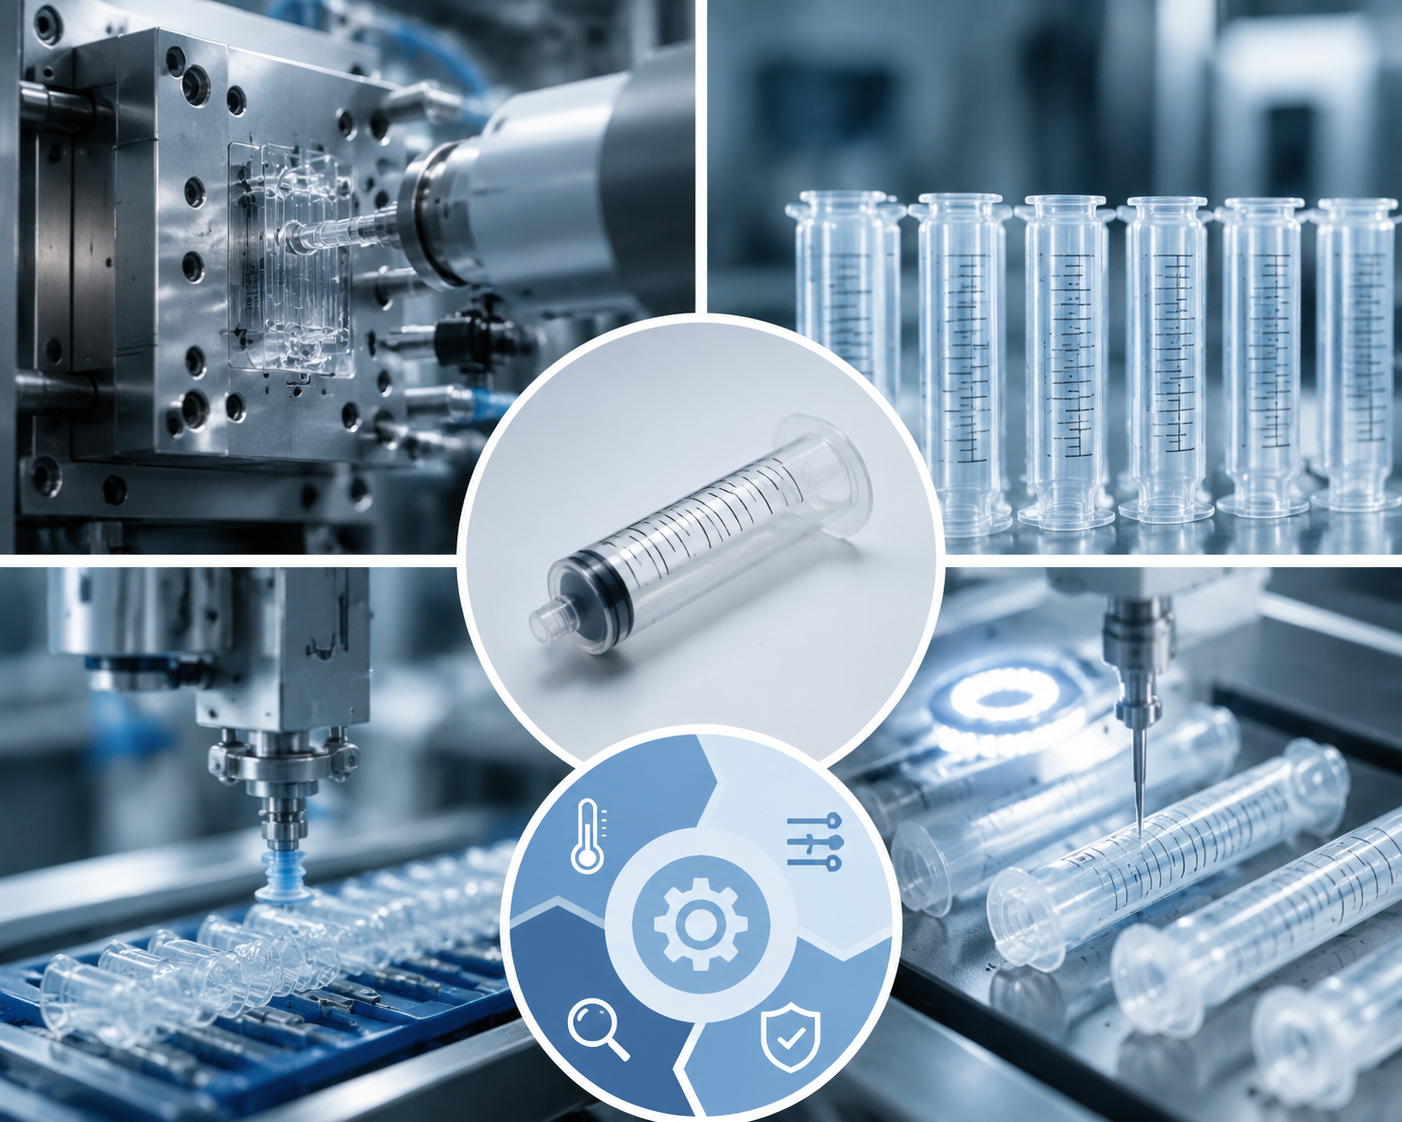 |
The component under analysis is a standard 5ml medical syringe barrel molded from medical-grade transparent polypropylene (PP). This specific material is formulated to withstand gamma ray sterilization and exhibit low extractable/leachable profiles, ensuring complete safety when in contact with pharmaceutical fluids.
From a structural standpoint, the syringe barrel is a cylindrical, thin-walled precision part with incredibly strict dimensional constraints:
Wall Thickness: Only 0.6mm (extremely thin-walled).
Total Length: 78mm.
Inner Diameter Tolerance: Controlled tightly within 0.02mm.
Barrel Roundness: Must be within 0.015mm.
To pass stringent medical certifications, the molded parts must meet four core operational criteria:
Ultra-Smooth Inner Wall: The internal surface must be completely free of scratches, weld lines, or gate vestigies to ensure the rubber plunger slides smoothly without resistance or stiction.
Flash-Free and Burr-Free Appearance: The exterior must have absolutely no flash or burrs, eliminating any risk of sharp edges puncturing surgical gloves or scratching healthcare workers.
Sterilization & Purity Compliance: The final product must withstand Ethylene Oxide sterilization without degrading. Furthermore, the molding process must not cause any molecular degradation or precipitation of harmful substances that could contaminate the medication.
Automation Compatibility: The mold must be designed for direct, gate-free removal via automated robotic arms. Eliminating manual gate trimming ensures maximum production efficiency and maintains a cleanroom environment.
The inherent material properties of medical-grade transparent PP directly dictate the injection molding parameters and mold design strategies.
| Material Property | Process Impact & Engineering Solution |
| High Shrinkage Rate (1.6% – 1.8%) | PP exhibits high and highly directional shrinkage. The precision mold cavities must feature segmented dimensional compensation based on specific zones to prevent the final product from falling out of tolerance. |
| Excellent Flowability vs. High Shear | While PP melts flow easily, filling a 0.6mm thin wall requires high-speed injection. This can generate excessive shear stress and visible weld lines, which compromise both the structural integrity and optical clarity of the barrel. |
| Thermal Sensitivity | Medical PP degrades easily if held at high temperatures for too long. If the hot runner system’s temperature control fluctuates, thermal decomposition occurs, releasing small-molecule extractables. Precise, localized hot runner temperature control is mandatory. |
| Cooling Deformation Tendency | During the cooling phase, any uneven thermal dissipation will cause the barrel to warp or become elliptical. This immediately violates the 0.015mm roundness spec. A highly balanced, conformal cooling system is required. |
When scaling up to a high-cavitation precision mold (e.g., 32 or 48 cavities), several defects are likely to occur if the process is not fully optimized.
If the runner layout or hot runner manifold is poorly balanced, different cavities will experience variations in filling speed and packing pressure. This results in cavity-to-cavity weight discrepancies and inner diameter dimensional deviations, making stable mass production impossible.
If the cooling channels are improperly distributed or the cooling rate fluctuates across the core and cavity inserts, the syringe barrel will experience localized thermal stress. This leads to warpage and roundness values exceeding the 0.015mm threshold, causing the plunger to fit poorly or leak.
Filling a 0.6mm thin-walled part requires rapid injection speeds. If the mold’s venting system is inadequate, the air inside the cavity cannot escape quickly enough. It becomes highly compressed, causing localized overheating that leads to burn marks, material degradation, or incomplete filling (short shots).
If the mold's parting surfaces do not match perfectly, or if the clamping force is insufficient to resist the high injection pressures required for thin-walled molding, micro-flash and burrs will form along the edges. This violates medical safety guidelines and introduces a scraping hazard.
Because the barrel wall is only 0.6mm thick, utilizing a standard single-point or poorly distributed ejection system will concentrate too much force on a localized area. This causes wall dimpling, structural stress whitening, or permanent deformation upon part stripping. A synchronized sleeve or stripper-plate ejection mechanism is critical to distribute force evenly.
 EN






 Hot News
